Discover how SMC is applying the 4BAR factory concept to improve visibility, optimise compressed air usage and uncover new opportunities for efficiency.
 By Mário Jakubec, Facility and Development Manager, SMC Czech Republic
SEPTEMBER 2026
Compressed air is often one of the most important utilities in a manufacturing facility, yet it is rarely questioned in the same way as production processes, machine performance or energy consumption.
The 4BAR factory principles are already being applied in selected SMC manufacturing facilities.
At SMC's European central production facility in Vyškov, Czech Republic, we applied the approach within our own production environment to better understand how compressed air was being used, where losses occurred and which opportunities for improvement existed.
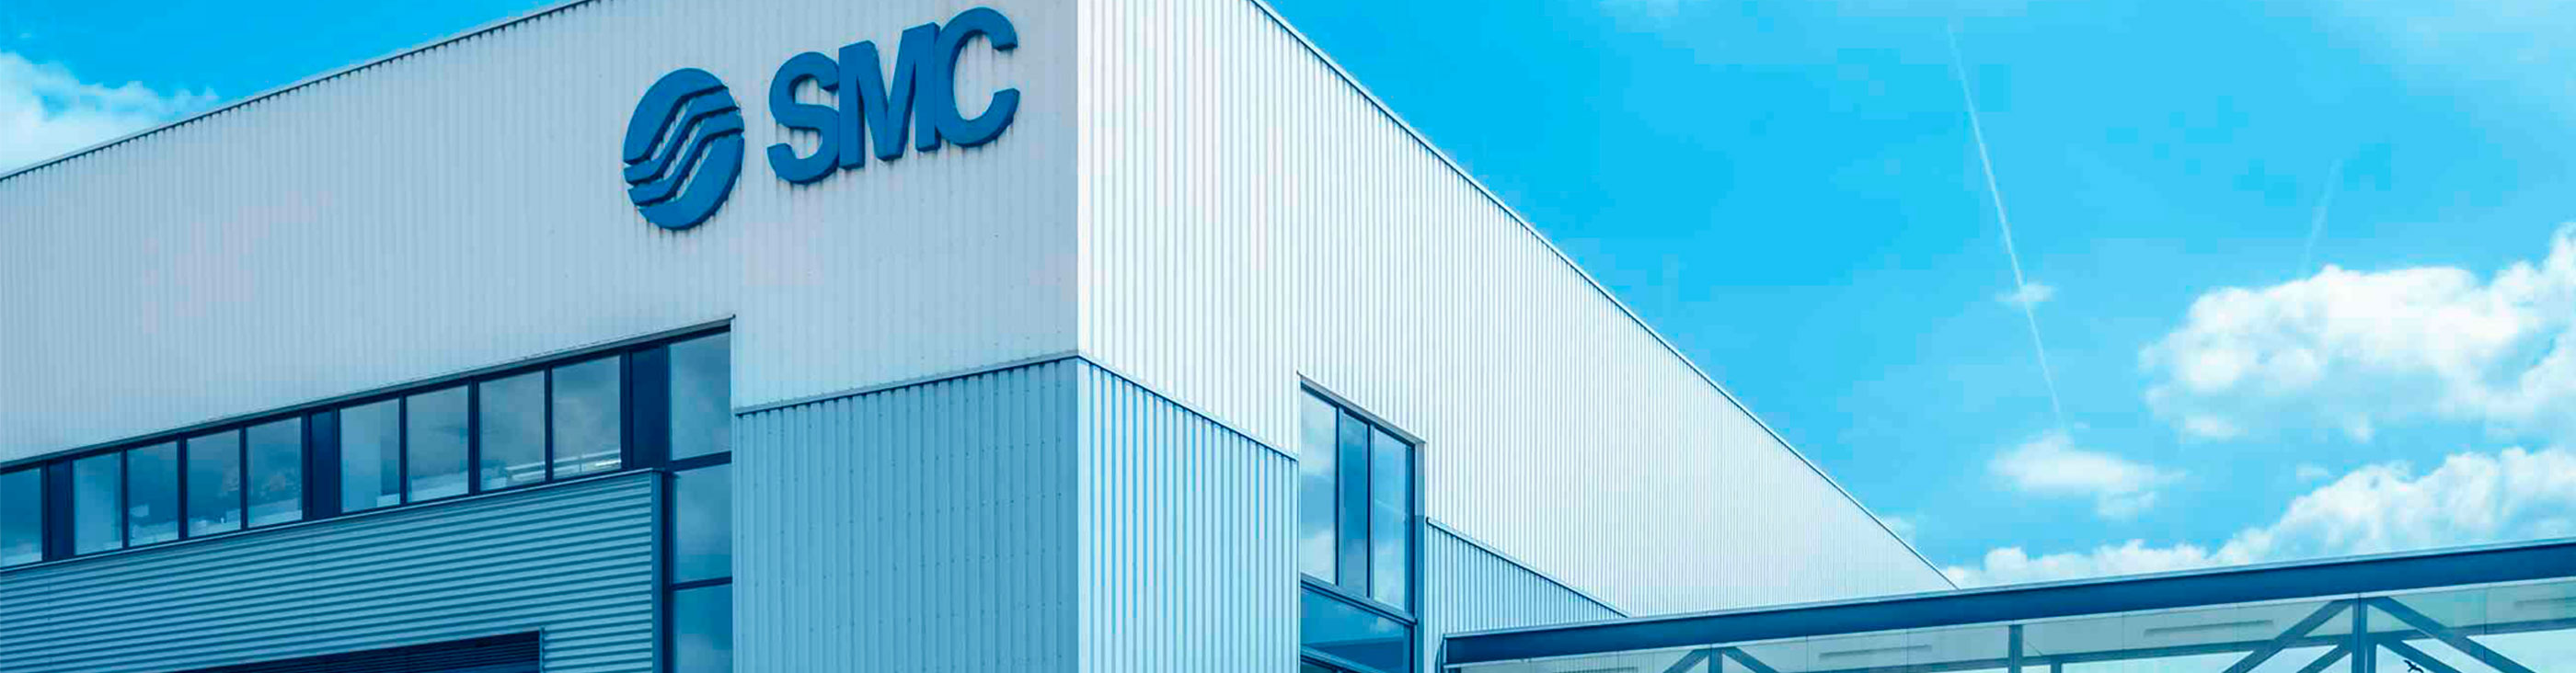 SMC's production facility in Vyškov, Czech Republic
By combining measurement, analysis and continuous optimisation, we turned compressed air consumption into visible, measurable data and used those insights to support more efficient factory operation.
What the journey towards a 4BAR factory involves
The 4BAR factory concept is often associated with pressure reduction. However, the approach goes far beyond simply lowering pressure.
One of the first objectives was to understand which machines could reliably operate at 0.4 MPa (4 bar), which applications required additional support technologies, such as pressure boosters, and which were not yet ready for conversion.
Measuring before improving
Working on the principle of “Data rather than assumptions”, the first step was to establish a clear understanding of how compressed air was being used across the factory.
To do this, we identified 70 machines with the greatest potential for analysis and improvement. Monitoring equipment is currently being installed on 54 of them. This provided visibility across 77% of the equipment included in this phase of the project.
The data gathered allowed our technicians to compare consumption levels, identify deviations and verify whether operating pressures are appropriate for each application. Most importantly, it provided the information needed to make decisions based on facts rather than assumptions.
Scalable monitoring architecture
As monitoring coverage increased, wireless communication was adopted to simplify deployment across the machine shop.
Compared with a conventional wired installation, the solution eliminated the need for approximately 4,000 metres of cabling, reducing implementation costs by around €10,000 and saving approximately 128 hours of installation work.
The result was a scalable monitoring architecture capable of being expanded efficiently within an operating production environment.
Air Management System: turning data into action
In addition to supporting long-term optimisation, continuous monitoring provides valuable diagnostic capabilities by making abnormal operating conditions immediately visible.
At SMC Vyškov, the Air Management System detected a seven-fold increase in compressed air consumption on one CNC machine. By analysing the available data, the team quickly identified the root cause: a faulty feed valve.
The issue was resolved in approximately one hour, preventing unnecessary compressed air losses that could otherwise have remained unnoticed for an extended period.
This example demonstrated one of the key strengths of our Air Management System and the 4BAR factory approach: transforming compressed air from an invisible utility into a measurable and controllable resource.
Lower pressure, same performance
In industrial environments, it is common for machines to operate at higher pressures than necessary. Every unnecessary additional bar increases the energy demand placed on the compressor room, raises operating costs and places additional strain on the compressed air infrastructure.
By analysing the data collected during the monitoring phase, we were able to verify the minimum pressure required for reliable operation. The findings showed that 52 of the 70 selected machines could operate below 0.5 MPa, representing 74% of the equipment included in this phase of the project.
One example involved machining centres producing SMC's MB series pneumatic actuator. Evaluation of the operating conditions confirmed that process performance could be maintained at pressures between 0.4 and 0.5 MPa instead of the original 0.6 MPa, reducing compressed air consumption by up to 25%.
The findings confirmed a key principle of the 4BAR factory concept: operating pressure should be determined by actual process requirements rather than convention or historical settings.
 Analysis data was collected during normal machine operation
Eliminating unnecessary consumption during idle periods
Monitoring data also revealed compressed air consumption occurring when equipment was not actively producing.
On selected CNC machines, compressed air continued to be supplied during idle periods despite no process demand being present. To address this, an automated shut-off valve was implemented to isolate the air supply whenever the machine is not operating.
This optimisation reduced compressed air consumption by approximately 75,000 m³ per year.
A similar opportunity was identified on another machine, where a probe air blow function operated continuously regardless of machine status. By linking the air blow directly to the machine sequence, compressed air is consumed only when the function is required, generating additional savings of approximately 108,800 m³ annually.
These examples demonstrate the importance of understanding not only how compressed air is used during production, but also how it is consumed when production is not taking place.
Designing for 4 bar
The project is not limited to optimising existing equipment. SMC Vyškov already specifies a working pressure of 0.4 MPa when defining requirements for new machines, helping ensure that future investments align with the principles of the 4BAR factory concept from the outset.
Turning experience into evidence
Many of the challenges addressed at SMC Vyškov are the same as those faced by manufacturing facilities worldwide.
By applying the 4BAR factory principles within our own operations, we are gaining practical experience under the same production conditions our customers face every day.
The project demonstrates that sustainable compressed air savings are often achieved through measurement, analysis and continuous improvement rather than major investment. Most importantly, it allows us to support customers with solutions that have been tested, validated and proven in our own manufacturing environment.


